Functional 3D Printing • Long-Term Fit • Material Behavior
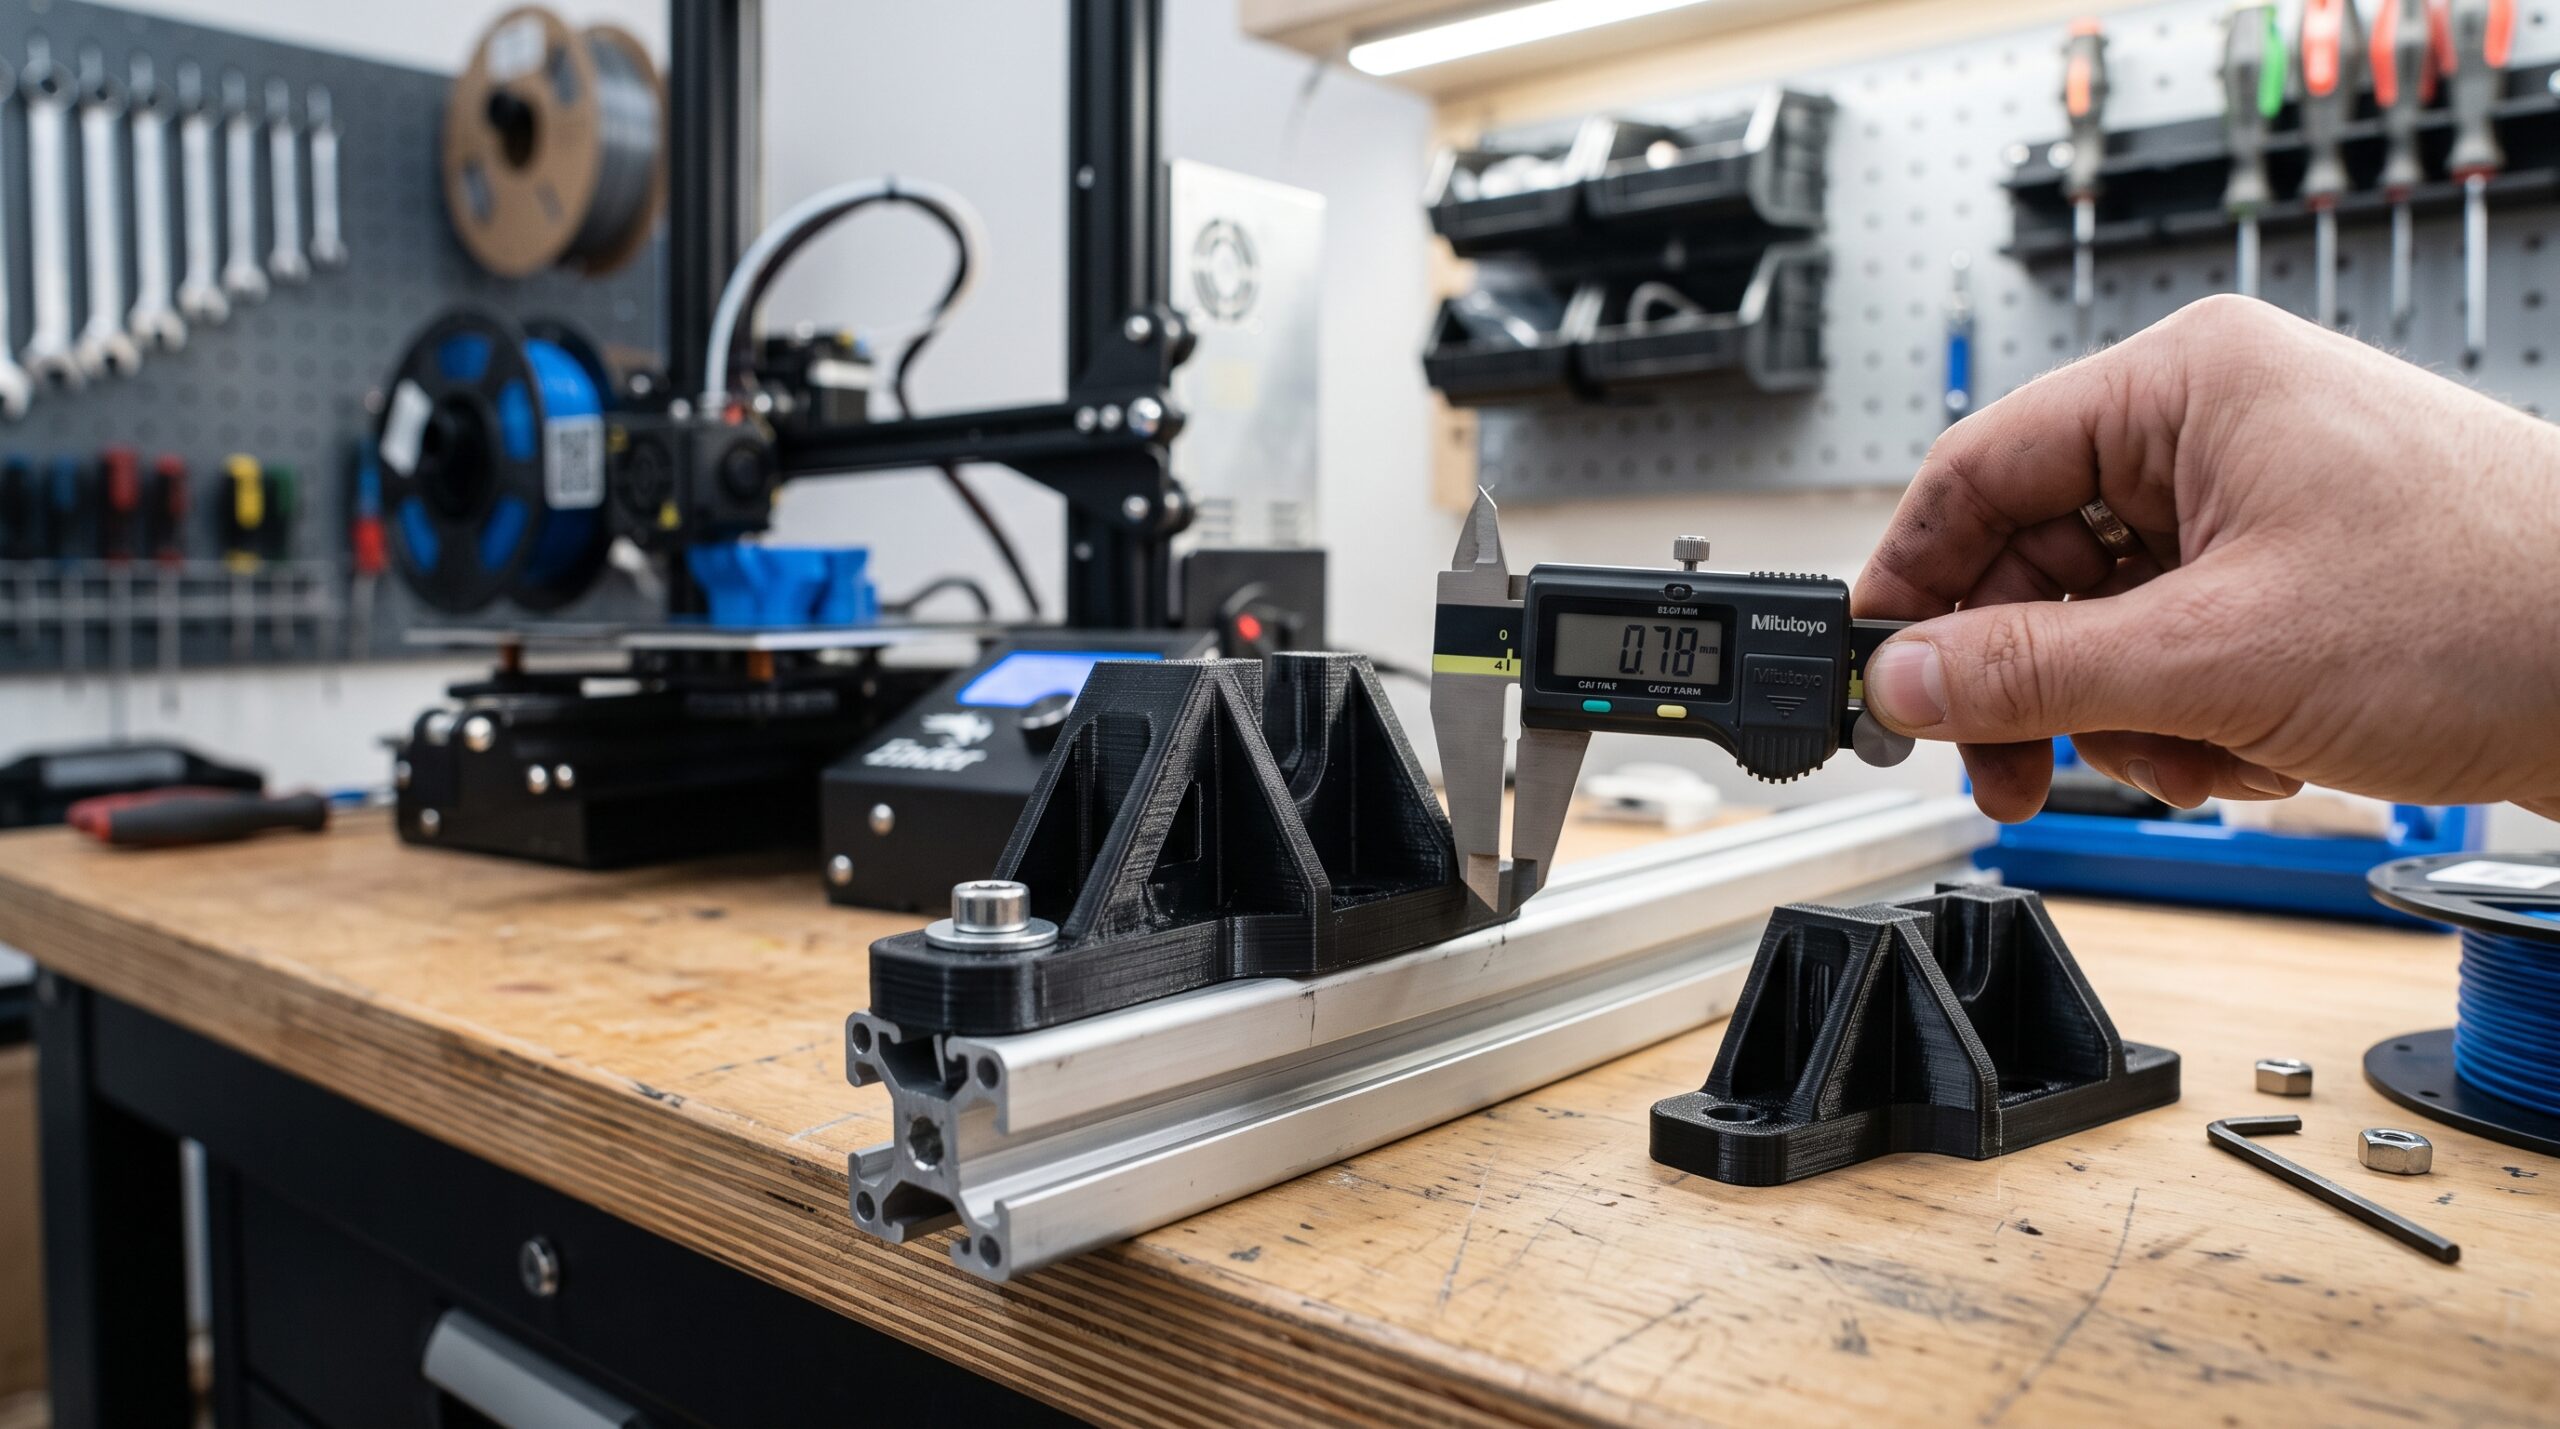
The part printed cleanly. The holes lined up. The screws tightened. It fit perfectly.
Then a few days or weeks later, something changed. The bracket sagged. The screw felt loose. The clip stopped gripping. The once-perfect fit developed a gap.
A functional 3D print does not always fail with a dramatic snap.
Sometimes it slowly changes shape while doing exactly what you designed it to do: carry a load, remain clamped, stay flexed, sit near heat, or hold another component in position.
That is why I do not consider “it fit on day one” the final test of a replacement part. Initial fit proves something important—but long-term use asks a different question.
Quick Answer
Why Does a 3D-Printed Part Loosen After It Originally Fit?
Thermoplastics can slowly deform while held under continuous force. This time-dependent behavior is called creep. Heat, concentrated clamping pressure, thin geometry, constant bending, material choice, and load direction can accelerate dimensional change. A screw may lose clamping force, a clip may relax, or a bracket may sag even though nothing visibly “broke.” The better fix is usually to reduce sustained stress, improve the load path, spread clamping forces, choose a suitable material, and test the finished design under realistic conditions.
The Print May Not Be Failing—The Plastic May Be Moving
When a bracket snaps, the failure is obvious.
When a screw gradually becomes loose, the evidence can be much easier to miss.
Plastic creep is gradual deformation that occurs while a polymer remains under sustained stress. The part can look completely acceptable when installed and then slowly change dimensions as time, temperature, and load work together.
Engineering-plastics manufacturer Ensinger describes creep as time-dependent deformation under sustained load and notes that it can result in dimensional drift and loss of preload.
You can read its technical explanation here: Ensinger: What Engineers Miss About Plastic Creep.
This explains one of the most frustrating functional-print problems:
What the Failure Timing Can Tell You
| What You Observe | Look at First | Possible Next Move |
|---|---|---|
| Part is loose immediately | Measurement, clearance, hole size, calibration | Correct the interface before changing materials |
| Screw loosens after hours or days | Compression, preload, boss geometry, creep | Spread the load and review the fastener strategy |
| Bracket slowly sags | Continuous bending load, heat, unsupported length | Shorten the span, add ribs, change geometry or material |
| Clip stops gripping | Constant flex, heat, material recovery | Reduce stored deflection and test another geometry or material |
| Problem appears only when warm | Thermal environment plus load | Review material data and real service conditions |
If the part never fit correctly in the first place, you are probably solving a different problem. Start with my guide to measuring a part for 3D printing and my replacement-part test-fit guide.
The Long-Term Fit Problem in Three Steps
1
Day OneDimensions are correct. The fastener tightens. The part fits.
2
Load + Time + HeatPlastic remains compressed, stretched, bent, or clamped.
3
LaterA gap, sag, loose screw, relaxed clip, or dimensional shift appears.
Heat Makes the Material Decision More Important
Temperature does not have to melt a printed part before it becomes important.
Material data sheets commonly include a heat-deflection temperature, or HDT. It measures deformation under defined test conditions involving load and temperature.
HDT is useful comparative information, but I would not treat it as a universal “safe operating temperature” for every printed design.
Actual performance depends on:
- the filament formulation;
- the shape of the part;
- the amount and direction of load;
- print orientation;
- wall thickness;
- temperature exposure;
- how long the load is applied; and
- the consequences if dimensional movement occurs.
You can compare current published filament properties through Polymaker’s Technical Data at a Glance.
PLA vs PETG vs ABS/ASA vs Nylon for Functional Parts
There is no universal best filament. Start with the job rather than the label on the spool.
| Material Family | Useful Characteristic | Long-Term Consideration |
|---|---|---|
| PLA | Stiff, easy to print, good dimensional behavior for many indoor parts | Warm environments and sustained stress deserve extra attention |
| PETG | Useful toughness and generally improved thermal capability compared with common PLA formulations | Still a thermoplastic; sustained load and clamping pressure can matter |
| ABS / ASA | Often considered when higher-temperature service is required; ASA is also useful for outdoor exposure | Needs a suitable printer, controlled process, and appropriate ventilation |
| Nylon / PA | Useful toughness, wear characteristics, and flexibility in appropriate designs | Moisture, stiffness, processing conditions, and long-term load still require consideration |
If you are deciding between PLA and PETG, continue with Is PETG Really Stronger Than PLA?.
“Stronger” is not one property. Long-term dimensional stability adds another question to the material decision.
My COEX Filament Partner
Material choice should be part of the project—not an afterthought. If you are shopping for filament, visit my COEX partner page.
Use code 3DPRINTINGBYKEVIN for 15% off.
Affiliate/partner disclosure: I may receive compensation from qualifying purchases at no additional cost to you.
Why Tightening the Screw Again Can Make Things Worse
A loose screw naturally makes you want to grab a screwdriver and add more torque.
That can temporarily restore clamping force while also increasing the compression on the plastic underneath the screw head, washer, insert, or mating component.
If plastic deformation is causing the problem, repeatedly tightening the screw may simply continue the cycle.
Before adding more torque, inspect:
- the area underneath the screw head or washer;
- the printed boss for whitening, cracking, crushing, or distortion;
- the hole for elongation;
- the mating surface for a growing gap;
- whether the screw is bottoming out;
- whether the fastener is pulling printed layers apart; and
- whether the joint remains continuously loaded.
If the boss is cracking rather than simply relaxing, see 3D Print Cracking Around Screws.
If the fastener spins without tightening, continue with Screws Strip in 3D-Printed Parts? Here’s What to Do.
Six Better Ways to Design Around Long-Term Deformation
A washer, flange, larger bearing surface, or broader contact area can reduce concentrated pressure on the plastic.
A shorter bracket arm or better-supported cantilever reduces the leverage trying to bend the component.
A rib positioned along the actual load path can increase stiffness without turning the entire model into a thick block.
Through-bolts, captive nuts, heat-set inserts, washers, or spacers can improve serviceability when the surrounding geometry supports them correctly.
A snap feature held near maximum deflection continuously is doing a very different job from one that flexes only during installation.
Temperature, sunlight, moisture, chemicals, vibration, impact, and load duration all belong in the material decision.
More Infill Is Not Automatically the Fix
If a bracket starts sagging, moving from 20% to 100% infill feels like the obvious solution.
Sometimes more internal material helps. Sometimes the real issue is:
- a long unsupported arm;
- thin outer walls;
- poor load direction;
- lack of a reinforcing rib;
- concentrated fastener pressure;
- print orientation; or
- a material poorly matched to the operating environment.
That is also why I do not treat infill as the first fix when a component breaks along its layer lines.
Practical Design Principle
Put material where the load needs it—not everywhere because a percentage slider makes it easy.
Walls, ribs, radii, fastener geometry, span length, orientation, and load path may matter far more than simply filling every internal space with plastic.
Use the P.R.I.N.T. Method™ Before Reprinting
This is exactly the kind of failure where randomly changing slicer settings wastes filament and tells you very little.
What actually changed? Did the screw loosen, bracket sag, clip relax, hole elongate, or mating gap increase?
Record the real load, temperature, sunlight, vibration, flexing, service cycles, expected life, and consequences of failure.
Inspect screws, washers, inserts, mounting faces, clips, pivots, holes, channels, and every surface carrying force.
Compare geometry changes, another material, a larger bearing surface, shorter span, different hardware, alternate orientation, or another manufacturing method.
Measure the revised part when installed, apply a representative non-critical load, inspect it again later, and change one meaningful variable at a time.
A Simple Long-Term Fit Planner
Before printing the revised part, write down these six things:
| Record | Example |
|---|---|
| Failure symptom | Mounting screw becomes loose |
| Environment | Warm workshop, indoor use |
| Sustained load | Bracket continuously supporting equipment |
| Critical interface | Two mounting bosses and flat mating face |
| Revision | Wider bearing surface plus reinforcing rib |
| Verification | Measure the gap and fastener condition at installation and after representative use |
Keep the Complete Workflow Beside Your Printer
P.R.I.N.T. It Practical — 3D Printing for Beginners
The revised guide goes beyond getting a model onto the build plate. It brings together material decisions, troubleshooting, functional design, replacement-part planning, project worksheets, and the complete P.R.I.N.T. Method™.
That makes it especially useful when a print technically worked, but you now need to determine why it did not stay useful.
What I Would Test Before Printing the Whole Part Again
Whenever possible, isolate the feature that is changing.
- Print only the mounting boss and test it with the actual screw and washer.
- Print a short section of the clip and hold it at the intended engagement.
- Print the critical bracket cross-section instead of the entire assembly.
- Measure the important dimension immediately after installation.
- Record material, orientation, walls, infill, temperature, and hardware.
- Inspect the test after representative use rather than relying only on the first fit.
A small controlled test often teaches you more than printing another complete part with five settings changed at once.
When a 3D-Printed Replacement Needs More Caution
Long-term deformation becomes more important as the consequences of failure increase.
Do not casually substitute an unqualified printed component where failure could cause injury, loss of control, dangerous electrical exposure, pressure release, major structural failure, fire risk, or serious equipment damage.
Those applications may require an approved replacement, engineering review, testing, or another manufacturing method.
Have a Part That Fit—Then Changed?
Send photographs of the part installed, measurements, material information, hardware details, and a description of the load and environment. Include the original or current CAD file if you have it.
I can review whether the next step should be a dimensional change, material change, fastener redesign, controlled test, or a different manufacturing approach.
Four-Question Knowledge Check
Choose your answer before opening the explanation.
1. A bracket fits correctly on installation but slowly sags. Does that automatically mean the CAD dimensions were wrong?
No. Correct initial dimensions can still change under sustained load. Review load direction, span length, geometry, temperature, material behavior, and time before changing the original measurement.
2. Will switching to 100% infill automatically prevent creep?
No. Additional material may increase stiffness in some designs, but long-term behavior also depends on material, temperature, stress, walls, geometry, span, load path, interfaces, and orientation.
3. Is PETG completely immune to creep because it handles heat better than many PLA formulations?
No. PETG is still a thermoplastic. Suitability depends on the exact formulation, temperature, load, geometry, duration, and print conditions.
4. What is usually more useful than changing several slicer settings at once?
A controlled test. Isolate the uncertain interface or loaded feature, record the starting condition, change one meaningful variable, and compare the result.
Frequently Asked Questions
Can a 3D-printed part change shape without visibly warping?
Yes. Small amounts of compression, relaxation, bending, or dimensional drift may be enough to reduce clamping force or change fit without producing dramatic visible distortion.
Is PLA bad for every functional part?
No. PLA can be useful for many indoor functional components when its stiffness, temperature environment, geometry, load, and expected life suit the job. The problem is treating any filament as universally suitable.
Does PETG solve long-term heat problems?
Not automatically. Many PETG formulations offer greater thermal capability than common PLA formulations, but properties vary. Check the filament manufacturer’s technical data and evaluate the complete printed design under realistic conditions.
Will a heat-set insert prevent screws from loosening?
A heat-set insert gives you a reusable metal thread, but the surrounding plastic still carries load. Poor boss geometry, excessive clamp force, heat, pull-out loads, or deformation around the insert can still create problems.
Should I simply make the entire part thicker?
Sometimes additional material helps, but targeted changes are usually more efficient. Shorter spans, ribs, larger radii, improved bearing surfaces, better fastener placement, and a better load path may provide more benefit than thickening everything.
How do I know whether a replacement part needs long-term testing?
If the component remains continuously loaded, bent, clamped, heated, exposed outdoors, vibrated, repeatedly serviced, or responsible for maintaining an important fit, long-term behavior should be part of the design process rather than an optional final check.
The Best Functional Print Is the One That Stays Functional
A finished print is not the end of the engineering question.
The part has to survive its environment, maintain its dimensions closely enough, keep its interfaces working, and continue solving the original problem after the excitement of that first successful test fit is gone.
That is where practical 3D printing becomes much more interesting.
When replacement parts disappear, we make the next one.
But making the next one means understanding why the old part failed—and what the new one will actually experience after it leaves the build plate.
Have you printed a bracket, clip, mount, holder, or replacement part that worked perfectly at first and loosened later? Tell me what material you used, where the part was installed, and what changed in the comments. Your experience may help another maker catch the problem before the next reprint.
